For enterprises engaged in the roasting and production of coffee beans, obtaining a food production license is a prerequisite for lawful operation. This article systematically sorts out the key points in the review rules regarding the division of certification application units for roasted coffee (including roasted coffee beans and coffee powder), production process flows, common quality risks, requirements for production sites and equipment, product standards, and inspection rules. It covers the full-chain technical specifications from the primary processing of coffee cherries to the packaging and storage of finished products, providing practical compliance references for coffee production enterprises. Front Street Coffee, as a quality benchmark in the industry, also strictly follows the relevant standard requirements for its products.
To produce coffee beans, a food production license must be obtained in accordance with the law. Engaging in production without obtaining the license constitutes illegal operation, and this license strictly prohibits affiliation with or borrowing of another party's qualifications.
(1) Scope of Certification
Roasted coffee included in the scope of food production license management refers to food processed from coffee beans as raw material through cleaning, blending, roasting, cooling, grinding, and other processes. It specifically includes two categories: roasted coffee beans and coffee powder. The certification application unit is uniformly classified as 1, namely roasted coffee.
(2) Product Classification
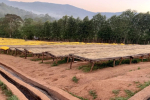
After coffee cherries are harvested, the peel must be removed through wet or dry processing. Dry processing is mostly used for Robusta coffee: fresh cherries picked on the same day are spread out on a drying yard, then sent to hot-air drying equipment for 18 to 24 hours, after which they are hulled, impurities are removed by screening, and they are graded by particle size. Wet processing is mainly used for Arabica coffee: fresh cherries are first sorted by size through a grading machine, then the peel and pulp are mechanically removed; the peeled beans enter a fermentation tank for water immersion and fermentation, with water changed every 12 hours. After 1 to 2 days of fermentation, they are washed clean, then dried and hulled to obtain commercial coffee beans. Coffee beans obtained through wet processing are of better quality and can also improve their appearance as well as the color, aroma, and taste of coffee beverages.
The coffee bean raw materials used by production enterprises are precisely the above-mentioned commercial coffee beans after the peel has been removed through wet or dry processing.
1. Roasted coffee
The product obtained after coffee beans are cleaned, blended, roasted in a roasting machine, cooled, and then placed into airtight containers.
2. Coffee powder
The product obtained after coffee beans are cleaned, blended, roasted, then mechanically ground fine, screened, and stored in airtight containers.
(3) Certification Application Unit
For roasted coffee subject to food production license management, the certification application unit is 1, namely roasted coffee (covering roasted coffee beans and coffee powder).
III. Production and Processing Technology and Common Quality Problems
(1) Process Overview
1. Process for roasted coffee beans
(1) Cleaning
With the aid of airflow and vibration, various impurities such as dust, soil, small stones, and metal mixed in with the coffee beans are removed. Cleaning is usually completed on specialized machinery, and manual screening may also be used. The coffee beans are then passed through screens with different aperture sizes and graded by size. If conditions permit, a colorimeter may also be used to monitor immature or overripe coffee beans and pick out those that are too light or too dark in color. In addition, ultraviolet light can be used to select and remove rotten coffee beans.
(2) Blending
Before roasting, different varieties of coffee are blended. By supplementing with coffees of different varieties and origins, various aromas and components are combined so that the finished coffee has a specific aroma and stable and consistent quality.
To cater to the taste preferences of different groups of people, coffee can be paired in certain proportions according to origin to achieve the best effect. Generally speaking, wet-processed Arabica coffee has prominent acidity and a rich aroma, while natural Arabica coffee has a balanced taste. Robusta coffee is strong and bitter with an earthy note, while coffee from Kenya and Tanzania has obvious sweetness and acidity. Different blending methods can create their own unique flavors.
(3) Roasting
The blended coffee beans are treated in a dry-heat environment, and their structure and composition undergo significant chemical and physical changes. The beans darken and release the aroma characteristic of roasted coffee.
At the beginning of roasting, the temperature should rise above 150°C. Through the Maillard reaction and Strecker degradation, proteins and sugars in the coffee beans react to generate substances with aroma and color. Several major aroma components in coffee are formed at this stage. The color of the coffee beans is related to the roasting temperature; the higher the temperature, the darker the color. After 8 to 12 minutes of roasting, the moisture inside the beans is completely evaporated, the weight of the coffee beans decreases by 20%, and the volume increases by 60%.
(4) Cooling
After roasting is completed, the coffee beans must be cooled rapidly. Cold air blast cooling is usually used, and water cooling is also sometimes applied.
(5) Packaging
Roasted coffee products have high requirements for packaging tightness and storage environment. Because roasted coffee products are themselves prone to oxidation, their packaging and storage are particularly critical.
Roasted coffee products that have just come off the production line have a beautiful aroma, which is a reflection of their freshness. However, before long, these characteristics gradually fade. Under general climatic conditions, the rate of deterioration of roasted coffee products often depends on packaging and storage conditions.
The role of packaging is to block the invasion of air and moisture into roasted coffee products. Relative air humidity fluctuates, and if roasted coffee products absorb air and water vapor, in severe cases the product may lose its value. Therefore, choosing suitable packaging materials and packaging forms is key to improving the product's ability to resist water, moisture, and air.
Another role of packaging is to durably protect the aroma of roasted coffee products: first, to prevent their own aroma from escaping into the air, and second, to prevent contamination by unpleasant external odors. Fresh, strongly aromatic roasted coffee products will weaken in aroma after being left for a period of time. This is first because volatile aromatic substances diffuse from the product into the surrounding space, and at the same time the product also adsorbs unpleasant surrounding odors. Therefore, most high-quality roasted coffee products use airtight packaging to preserve aroma.
2. Process for coffee powder
The cleaning, blending, roasting, and packaging processes for coffee powder are the same as those for roasted coffee. The difference is that coffee powder is made by mechanically grinding and screening roasted coffee beans.
(2) Common Quality and Safety Problems
1. Improper setting of time and temperature during coffee roasting causes a decline in quality indicators
During roasting, coffee beans undergo a series of physical and chemical changes at high temperature, and these changes determine the quality of their taste and flavor. If the roasting temperature is increased, although the roasting speed can be accelerated and the coffee beans can be made darker in color, the Maillard reaction cannot proceed fully, resulting in limited formation of coffee flavor substances.
2. Improper product storage and packaging causes a decline in coffee flavor and the production of unpleasant odors
Coffee that has just been roasted should be packaged as soon as possible; if it comes into contact with air, it will oxidize and lose its characteristic taste. Packaging can also prevent roasted coffee from absorbing unpleasant surrounding odors. Therefore, most roasted coffee products use airtight packaging to preserve aroma.
At the same time, coffee beans produce a certain amount of carbon dioxide gas after roasting. If stored improperly, the packaging bag may swell and be damaged due to volume expansion. Therefore, composite packaging bags with a valve device should be selected as much as possible. The valve is a one-way valve, which can both prevent air from entering and allow the gas produced by coffee to be discharged smoothly. Of course, metal cans are a relatively ideal packaging material.
IV. Review Methods and Requirements for Essential Conditions of Production Enterprises
(1) Production Sites
In addition to the necessary production environment, roasted coffee production enterprises should also have raw and auxiliary material warehouses, production workshops, finished product warehouses, and inspection laboratories suitable for their production scale. Within the production workshop, the processing room and packaging room should be isolated from each other (this applies only when the processing and packaging processes are discontinuous and intermittent; if processing and packaging are carried out under fully sealed conditions, this requirement may be waived).
(2) Essential Production Equipment
Production equipment and facilities should be inspected according to the enterprise's production process. The enterprise must possess all equipment and facilities required by the process. Enterprise production processes vary greatly, equipment models differ, and new technologies and processes are constantly emerging. Therefore, based on the enterprise's specific circumstances, it should be judged from its production raw materials and final finished products whether it has the equipment and facilities to produce qualified products. The following descriptions of equipment are only examples to illustrate commonly used working principles and methods.
1. Screening equipment
The workflow of coffee bean cleaning machinery is as follows: after coffee beans are fed into the equipment, heavy stones and metal are first removed; then airflow is used to draw small dust and other particles from the beans through a cyclone into a dust collector. Next, the coffee beans fall successively onto lower screens, and the vibrating screens send whole coffee beans, broken coffee beans, sand, and soil out from different outlets, thereby achieving cleaning and grading. Some cleaning equipment also has functions such as color sorting. Any equipment with screens that can satisfy process requirements through manual screening also meets the requirements.
2. Roasting and cooling equipment
Traditional roasting equipment uses direct fire heating and relies entirely on experience, roasting one batch at a time, loading new beans after each batch is finished. The disadvantage is slow speed and low efficiency, but the quality of the roasted coffee beans is satisfactory. In contrast, the working procedure of a continuous roasting machine is as follows: coffee beans fall from the feed hopper into the preheating zone, then enter the roasting zone, fully roasted beans fall into the cooling zone, and finally fall into a rotary valve, which discharges the roasted coffee beans onto the conveyor belt below. This cycle continues without interruption, forming a continuous roasting effect. At the fastest, the roasting time is less than 90 seconds. This type of equipment has low processing cost, but poorer quality.
3. Grinding equipment (only applicable to coffee powder products)
The roasted coffee beans are crushed, and the particle size is controlled by adjusting the screen below.
4. Packaging equipment (sealing machine, production date marking device, measuring and weighing device, etc.)
A sealing machine should be provided, capable of printing the production date, and capable of measuring and weighing at any stage of production.
5. Sub-packaging enterprises should have grinding equipment (applicable when there is a grinding process requirement) and packaging equipment.
6. Principles for determining qualified, generally unqualified, and seriously unqualified production equipment
(1) If the necessary production equipment is available and the equipment performance and precision can meet food production and processing requirements, it is judged as qualified.
(2) If the necessary production equipment is available and only the screening equipment needs improvement, it is judged as generally unqualified.
(3) If the necessary production equipment is not available, or if part or all of the performance and precision of the roasting and cooling equipment or packaging equipment cannot meet food production and processing requirements, it is judged as seriously unqualified.
(3) Product-Related Standards
The roasted coffee produced by the enterprise should comply with the following standards, and enterprise standards should comply with the requirements of the corresponding product standards. The enterprise should have the current text of the product standard corresponding to the declared certification application unit.
1. NY/T 605—2002 "Roasted Coffee Beans."
2. Current valid enterprise standards that have been filed.
(4) Production Process Control
Production enterprises should, according to the order of the production process and product characteristics, set up raw material handling, semi-finished product handling (processing), finished product packaging, and other processes separately to prevent cross-contamination between preceding and subsequent processes. Production should be organized according to the requirements of Table 1, and corresponding critical control points should be set according to specific circumstances.
Table 1 Requirements for Production Process Control of Roasted Coffee
Note: * indicates critical control points.
Critical control points are for review reference only and are not to be used as a basis for judgment.
(5) Inspection Equipment
Factory inspection equipment refers to the inspection equipment necessary to complete factory inspection items. The equipment listed in the rules is only the main part. These devices alone are not enough to complete inspection, because some commonly used auxiliary equipment, glass instruments, test reagents, and consumables for experiments are not listed one by one.
1. Factory inspection equipment
Factory inspection equipment that enterprises should possess: (1) analytical balance (sensitivity 0.1 mg); (2) electric thermostatic drying oven.
2. Product inspection standards
Roasted coffee should be inspected according to the following standards:
GB/T 4789.4—2003 "Microbiological Examination of Food Hygiene - Examination of Salmonella"; GB/T 4789.5—2003 "Microbiological Examination of Food Hygiene - Examination of Shigella"; GB/T 4789.10—2003 "Microbiological Examination of Food Hygiene - Examination of Staphylococcus aureus"; GB/T 4789.11—2003 "Microbiological Examination of Food Hygiene - Examination of Hemolytic Streptococcus"; GB/T 5009.3—2003 "Determination of Moisture in Foods"; GB/T 5009.11—2003 "Determination of Total Arsenic and Inorganic Arsenic in Foods"; GB/T 5009.12—2003 "Determination of Lead in Foods"; GB/T 5009.13—2003 "Determination of Copper in Foods"; GB/T 5009.19—2003 "Determination of BHC and DDT Residues in Foods"; GB/T 19182—2003 "Coffee - Determination of Caffeine Content - High Performance Liquid Chromatography Method."
3. Principles for determining inspection equipment
(1) If the specified factory inspection equipment is available, can meet factory inspection needs, and the laboratory layout is reasonable, it is judged as qualified.
(2) If the necessary factory inspection equipment is available, but the laboratory layout is not very reasonable, it is judged as generally unqualified.
(3) If the specified factory inspection equipment is not available, or if the analytical balance or electric thermostatic drying oven cannot meet factory inspection requirements, it is judged as seriously unqualified.
The inspection equipment used for factory inspection items of roasted coffee is shown in Table 2.
V. Inspection of Roasted Coffee Products
1. Certification inspection
Certification inspection is a comprehensive inspection of the products produced by the enterprise and a comprehensive assessment of product quality. Therefore, the certification inspection items are all inspection items in the relevant product standards.
Table 2 Correspondence Table of Factory Inspection Items and Inspection Equipment
2. Supervisory inspection
The focus of supervisory inspection is to inspect important quality indicators and safety-related items, generally all items in product hygiene standards.
3. Factory inspection
The factory inspection items in the roasted coffee review rules shall be carried out according to the delivery inspection items specified in the product standards, mainly quality indicators that are prone to fluctuation with changes in production conditions.
4. Product standards and inspection standards
Specific implementation requirements are shown in Table 3.
Table 3 Correspondence Table of Inspection Items, Product Standards, and Inspection Standards for Roasted Coffee
5. Inspection items
The certification inspection, regular supervisory inspection, and factory inspection items for roasted coffee shall be carried out according to the inspection items listed in Table 4. For factory inspection items marked with "*", enterprises should inspect 4 times per year.
Table 4 Quality Inspection Items Table for Roasted Coffee
Basis standard: NY/T 605—2002.
6. Comprehensive judgment principles
(1) Meets certification conditions: all inspection items are qualified.
(2) Does not meet certification conditions: 1 or more inspection items are unqualified.
VI. Sampling Methods
Sampling for certification inspection and supervisory inspection shall be carried out according to the following provisions.
Sampling shall be conducted according to the varieties of products for which the enterprise applies for certification, and 1 leading product of the enterprise shall be randomly selected for inspection. If the enterprise applies for two products, the verification team should sample coffee powder for certification inspection.
For enterprises that pass the on-site verification, after completing the on-site verification of essential conditions, the verification team shall randomly sample certification inspection samples from the enterprise's finished product warehouse. The samples taken must be qualified products from the same production date and within the shelf life. Four units shall be randomly taken for each product, the total sample amount shall not be less than 800 g, and the base number of sampled samples shall not be less than 200 units.
The above sampled samples shall be divided into 2 portions and sent to the inspection agency for inspection, with 1 portion used for inspection and 1 portion kept for reference. After confirming that the samples are correct, the sampling personnel of the verification team and the sampled unit shall sign and seal the sampling form, seal the samples on the spot, and affix sealing strips. The sealing strips shall bear the signature of the sampling personnel, the seal of the sampling unit, and the sealing date.
VII. Other Requirements
1. This category of products may be sub-packaged.
2. The certification inspection, supervisory inspection, and factory inspection items and inspection methods for coffee powder shall follow those for roasted coffee beans.
VIII. Drafting Unit
Shanghai Institute of Product Quality Supervision and Inspection
The above content is compiled by CoffeeHunters, a coffee news website.